About Us
Custom Industrial Cables Manufacturer
Engineered for Extreme Environments
RouLine engineers and manufactures custom industrial cable solutions for demanding applications in subsea
operations, mining equipment, elevators, reeling systems, robotics, and harsh environments.
Our Capabilities Cover
Subsea Cables, ROV Umbilical Cables, ROV Tethers, Neutral Buoyancy ROV Cables,
Cold-Temperature, Arctic Grade Cable, Corrosion-Resistant, and Oil-Resistant Cables
Reeling Cables, Festoon Cables, and Spreader Cables
Elevator Traveling Cables, Crane Cables, and Robotics Cables


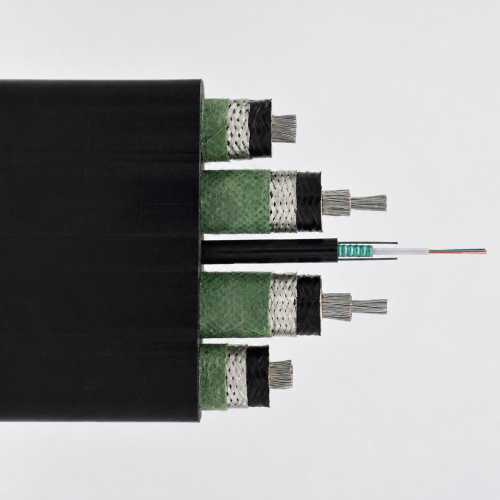
A selection of neutral buoyancy ROV Tether, Spreader Crane Cable A typical Subsea Umbilical Cable
Custom Engineering Capability
Engineering Cable Structures for Demanding Applications
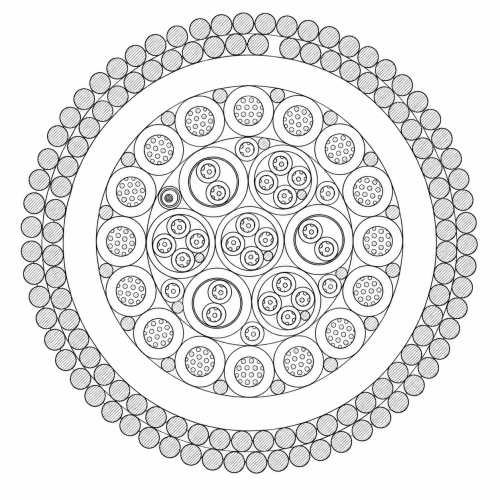 Every cable can be tailored in conductor structure, insulation system, shielding,
armouring, and jacket design to meet specific electrical, mechanical, and environmental
requirements.
With over 1,000 cable variants developed, RouLine engineering team works closely with
customers to create cable designs based on their application conditions, installation
methods, and system requirements.
From conductor configuration and electrical performance to mechanical protection and
environmental resistance, we provide customized cable solutions designed for each
customer's specific operating environment.
Cable Materials & Construction Capability
Every custom cable starts with the right material and construction
RouLine selects conductor, insulation, shielding, reinforcement and outer jacket materials according to the electrical,
mechanical and environmental requirements of each application.
Our material portfolio includes PUR, PVC, PTFE, FEP, PFA, PVDF, silicone, XLPE and LSZH compounds, enabling cable designs
for demanding environments requiring flexibility, abrasion resistance, chemical resistance, temperature performance and
long service life.
Materials are sourced from qualified suppliers, including established global material manufacturers, and evaluated
according to the requirements of the finished cable design.
① Conductor Materials
▶ Bare copper, tinned, silver-plated, or nickel-plated
▶ Alloys, pure nickel, thermocouple materials, and compensating materials
▶ Conductor cross-sections ranging from 0.00012 mm² to 500 mm²
Available in different conductor classes, strand constructions and cross-sections according to
electrical performance and flexibility requirements.
② Cable Stranding
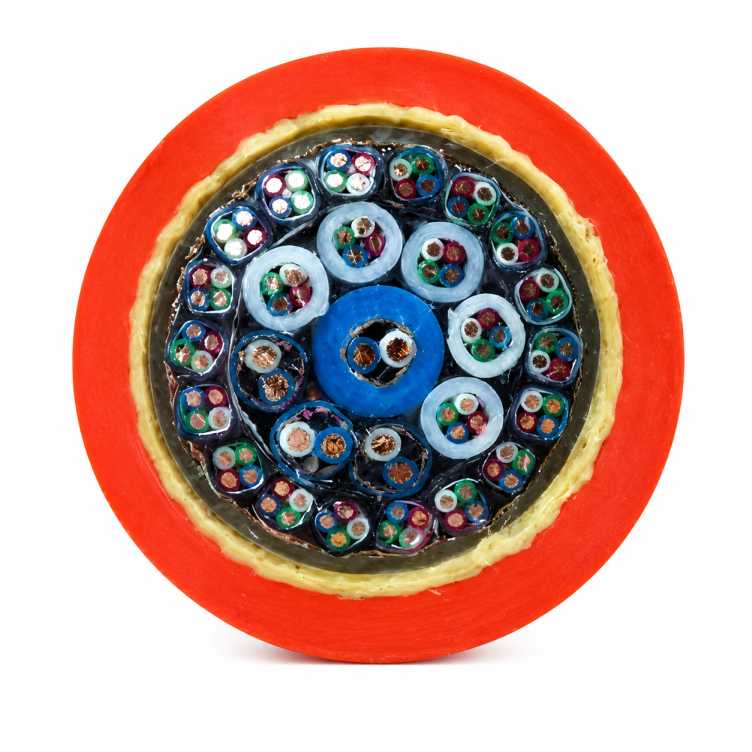
In multi-stranded and twisted-pair cables, the number of cores can range from 2 to 120 cores.
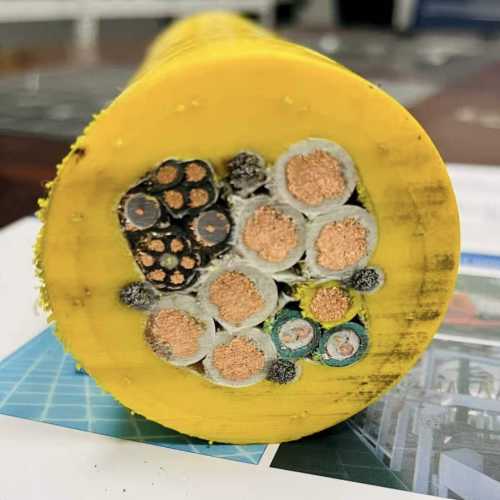
③ Insulation and Sheathing Materials
▶ Fluoropolymers: PTFE, PFA, MFA, FEP, ETFE, PVDF...
▶ Silicone Rubber: Standard compounds and custom application compounds
▶ Elastomers: EPDM, EVA...
▶ Thermoplastic Elastomers: TPE-U, TPE-E, TPE-S, TPE-O, TPE-V...
▶ Specialty Thermoplastics: PEEK, PI, PEI...
▶ Inorganic Materials:Fiberglass, mica, ceramic fibers...
▶ Fluoroelastomers: FKM
▶ Irradiation Cross-linked Materials: XVH, XL-PE...
▶ Thermoplastics: PA, PP, PVC, PE...
④ Tapes & Wrapping Tapes
▶ Films: PTFE, polyester, aluminum-laminated, copper, Kapton, and specialty materials
▶ Tapes: Fiberglass, mica, non-woven fabric
⑤ Shielding Materials
▶ Braided materials made of bare copper, tinned, silver-plated, nickel-plated, or specialty materials
⑥ Mechanical Reinforcement & Armoring 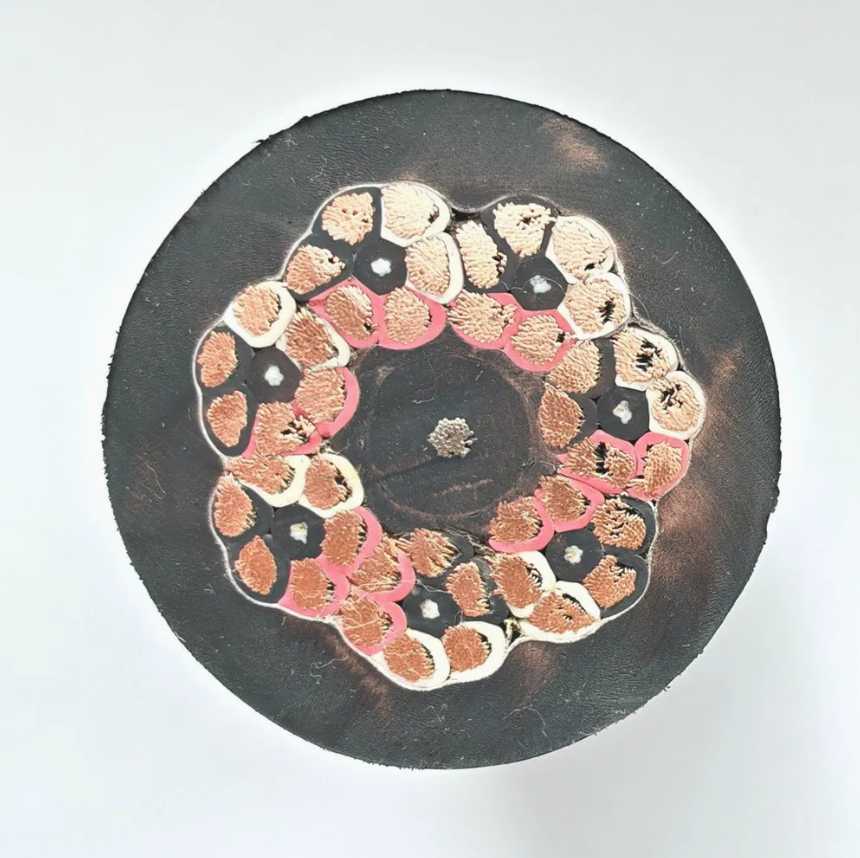
▶Metallic Armoring
Galvanized steel wire
Stainless steel wire
Other application-specific metallic reinforcement
▶Non-metallic Reinforcement
Aramid / Kevlar
Polyester
Other high-strength fibers
Manufacturing Process & Factory Environment
Flexible Manufacturing for Specialized Cable Designs
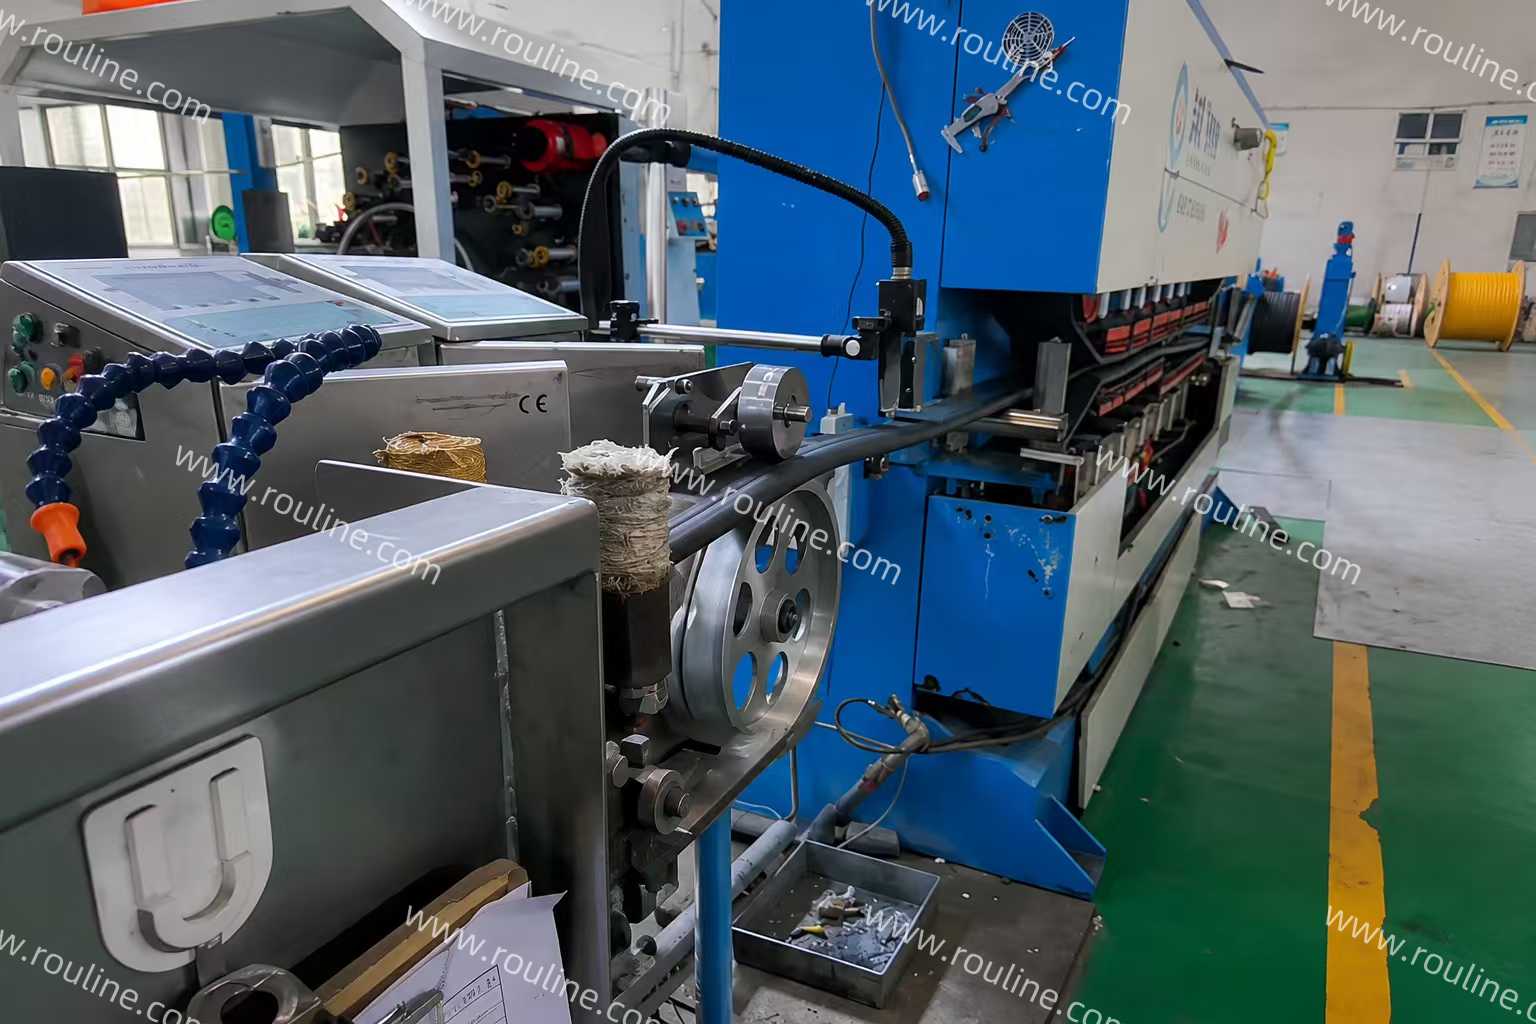
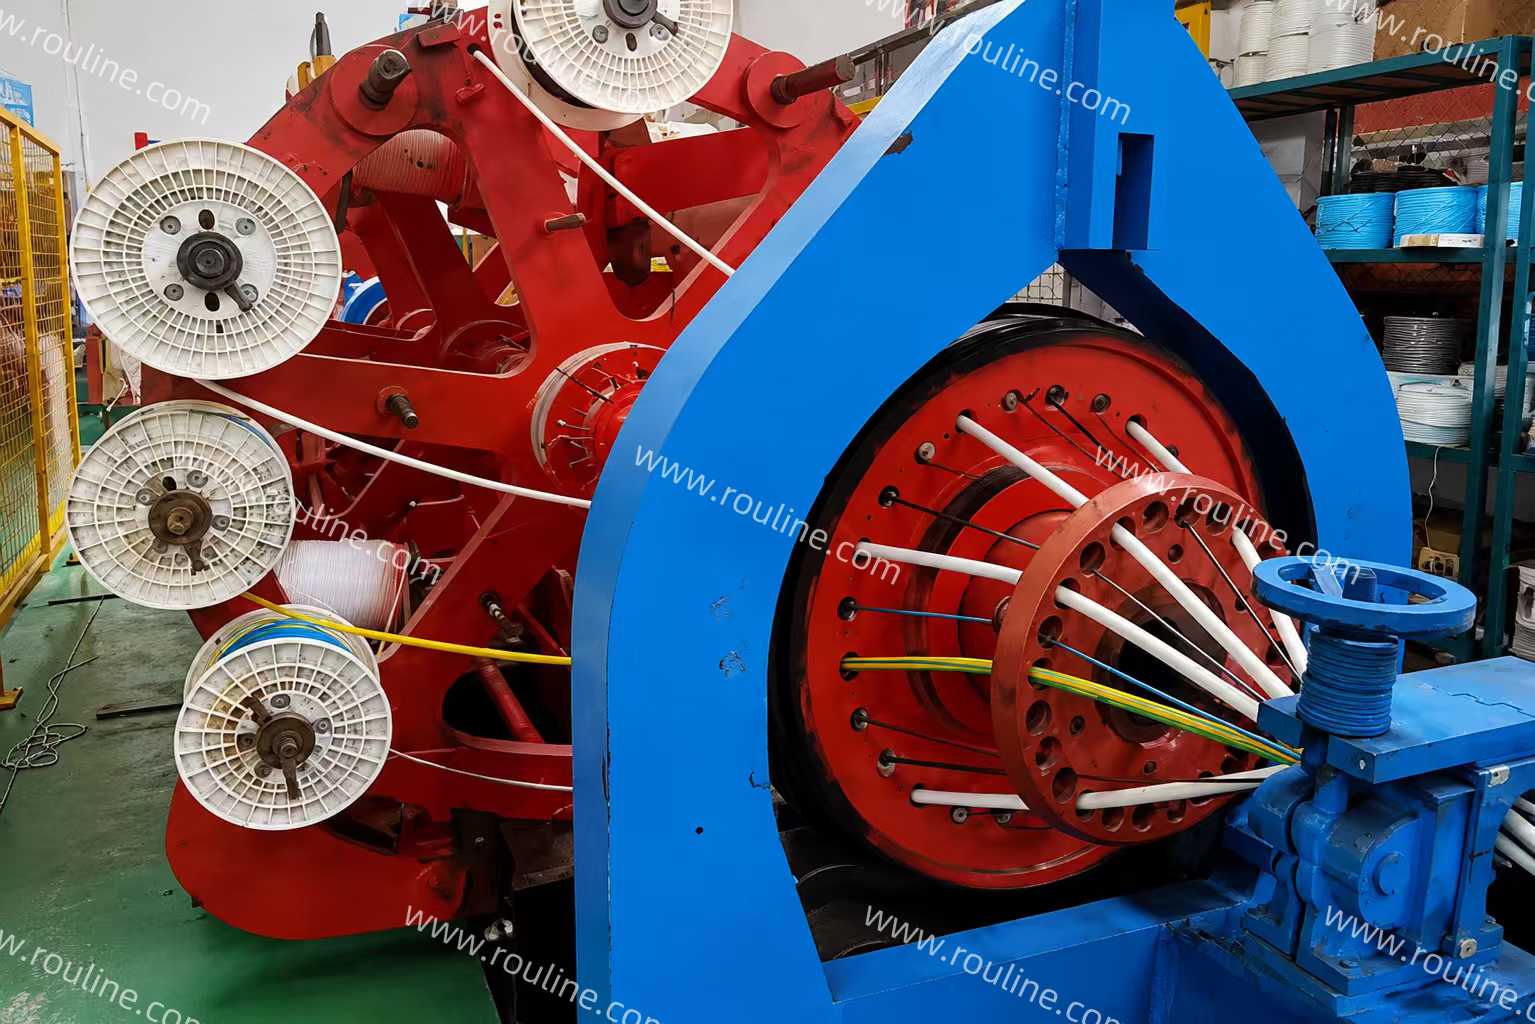
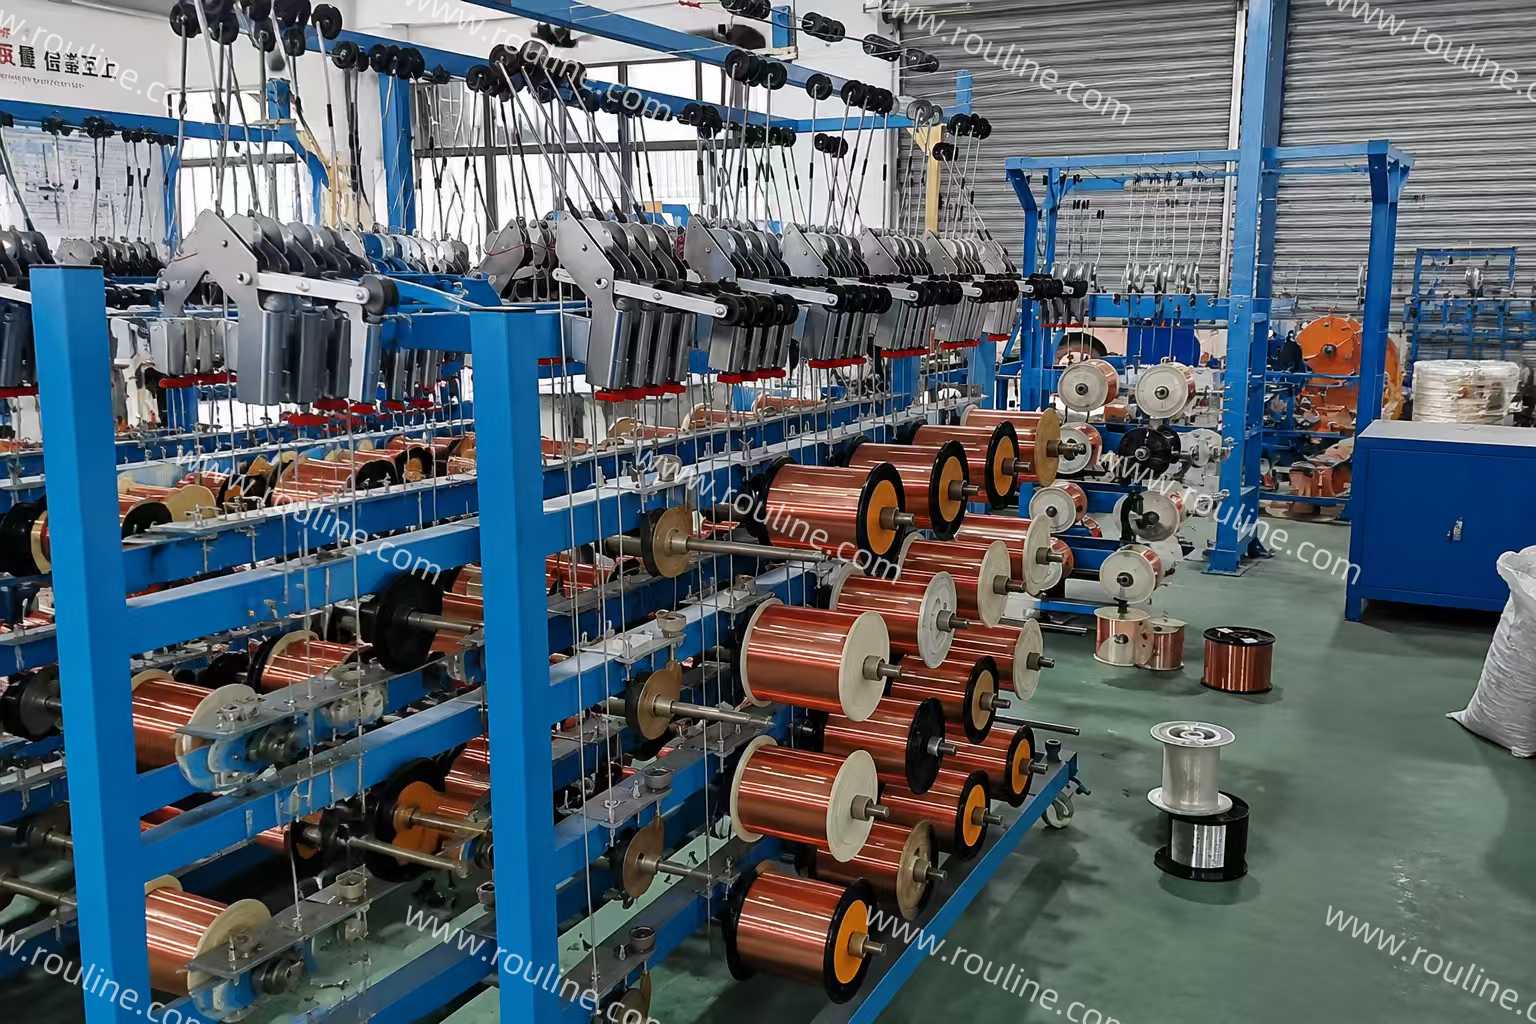
Our manufacturing process is built around the specific construction and application of each cable. From material preparation and
insulation extrusion to cabling, shielding, reinforcement, armoring, and final sheathing, production parameters are adjusted to
meet requirements for flexibility, mechanical strength, temperature resistance, chemical exposure, and demanding operating
environments. Our factory supports both customized cable production and small-batch manufacturing, with dedicated
equipment for different cable constructions. View Cable Gallery →


Testing & Inspection
Testing for Electrical, Mechanical & Environmental Performance
RouLine cable testing equipment supports routine and project-specific inspection throughout the manufacturing process.
Depending on cable construction and application requirements, testing may include electrical performance, insulation, continuity, tensile strength, environmental resistance, and dimensional inspection. Test methods and acceptance criteria can be adapted to the cable specification, applicable standards, and customer requirements. This testing process helps verify cable performance and manufacturing consistency before delivery. View More Equipments →

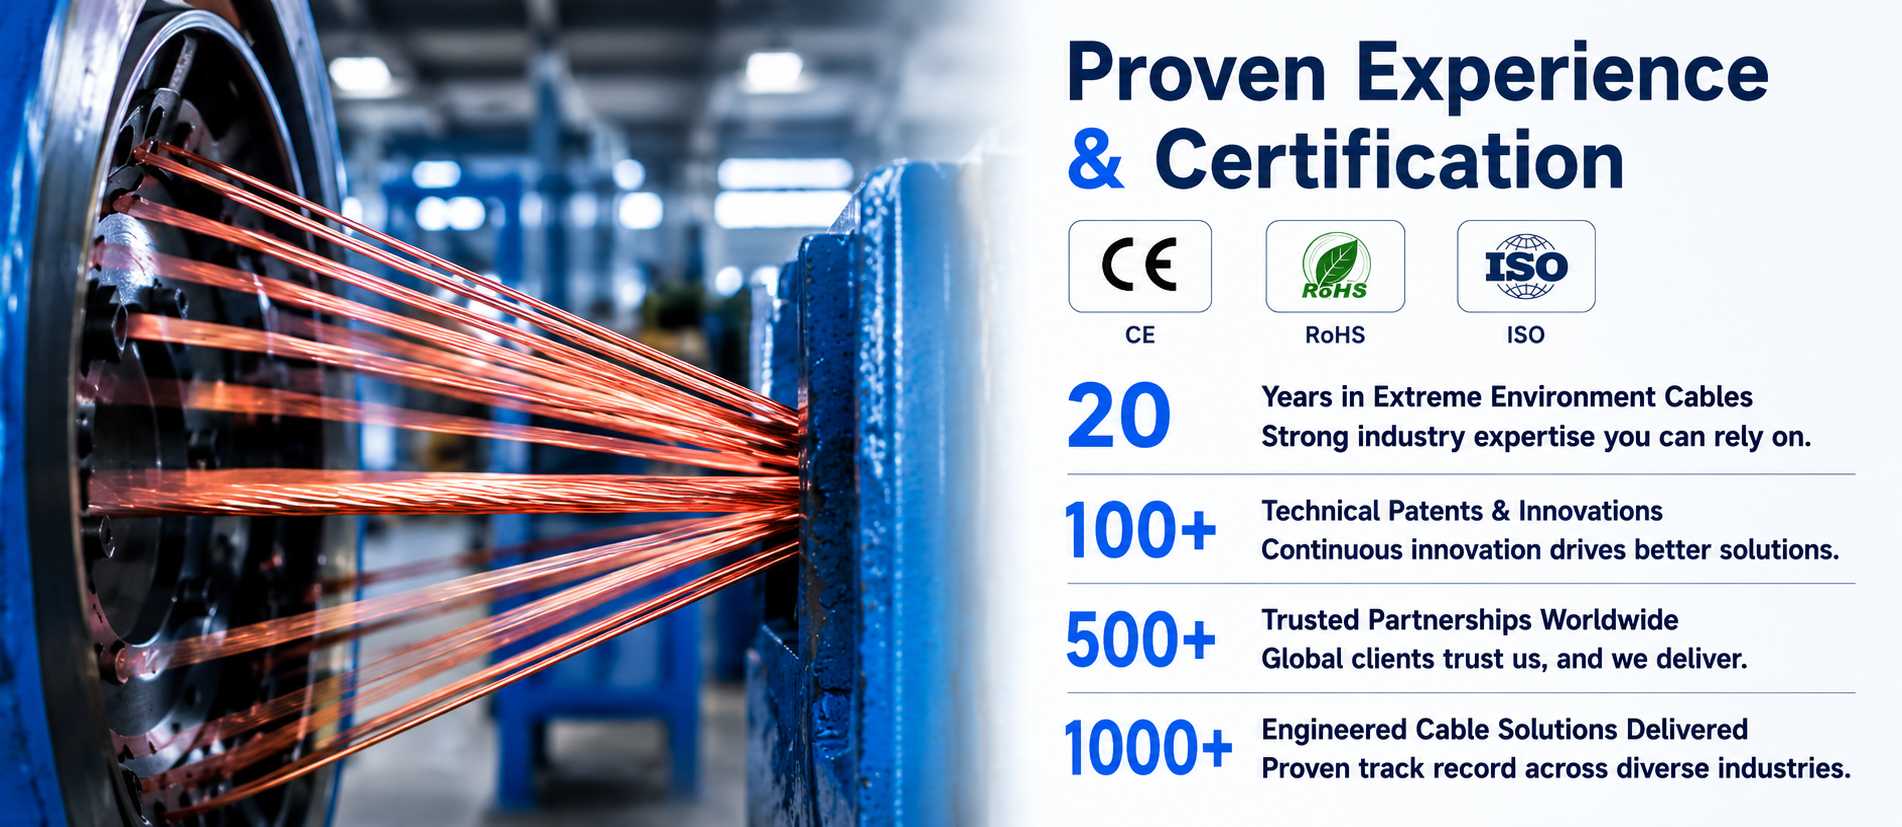
Proven Experience & Certification

Our Global Brands